Material, sub-suppliers and two production countries, managed as one plan — with country of origin as a decision, not an accident.
Having plants in both China and Vietnam is only useful if someone decides how to use them. We propose the production allocation against process, cost, lead time, country of origin and your export requirements — and then manage it.
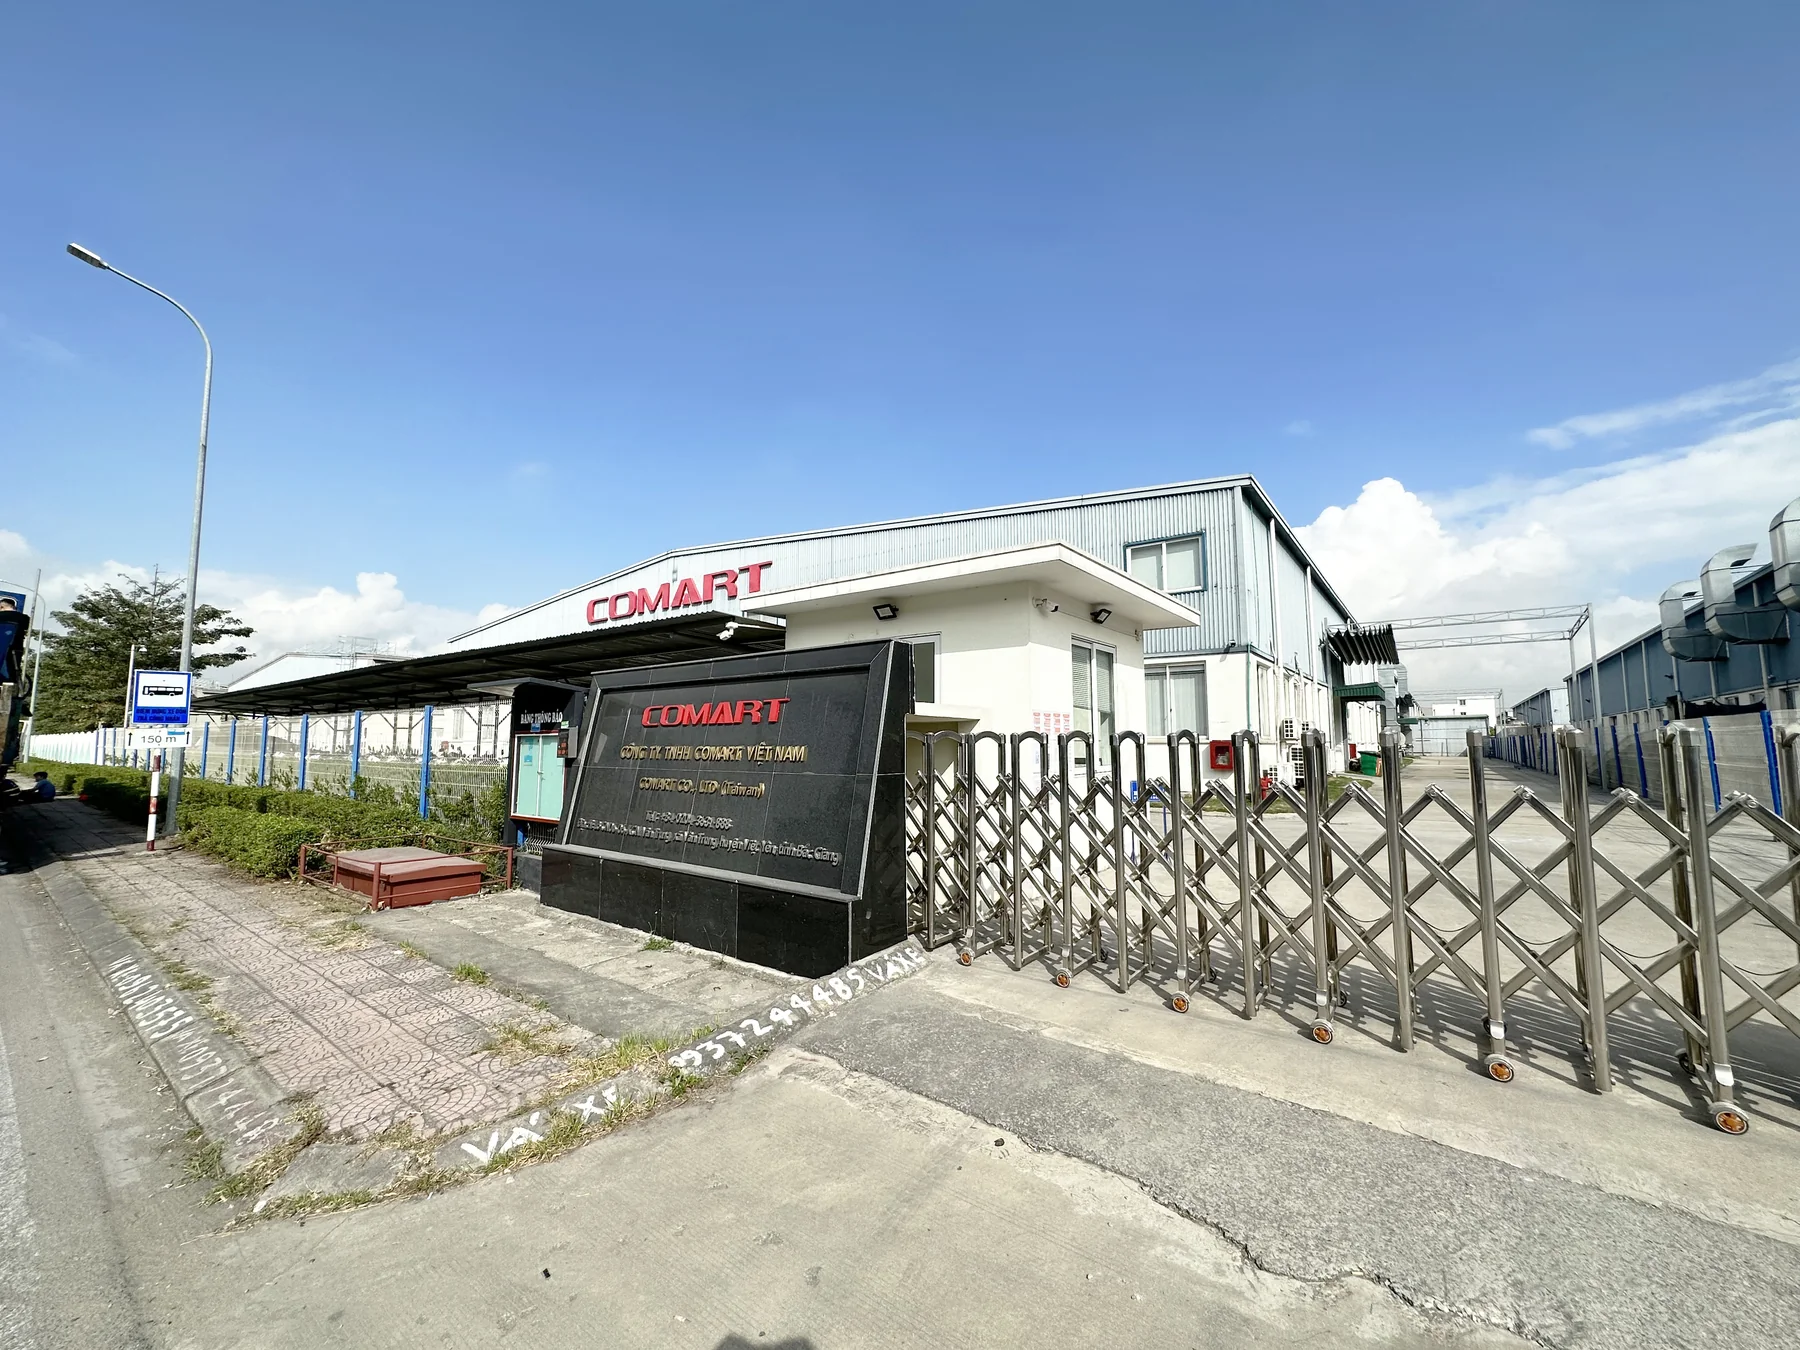
For customers shipping consumer accessories into the US and Europe, origin is frequently the deciding factor rather than unit price. Our Bac Ninh plant exists so that a mount or charging product can be made in Vietnam when tariffs, customer policy or a retailer's sourcing rules require it, without moving to a supplier you have never audited. Both plants run under one Taiwan-managed team, so the transfer is between our own sites rather than between two vendors.
Transfer from pilot run to mass production is treated as a controlled step with its own criteria, not as a date on a schedule.
Origin requirements, destination market and volume shape the production plan. Bring them early and the allocation is a decision rather than a constraint.